Vanway Precision Materials Tech Co.,Ltd
Common Specification Mistakes of 2020 Industrial Aluminum Extrusion Profiles
2020 Industrial Aluminum Profile Specification Guide: 7 Common Mistakes You Should Avoid
Table of Contents
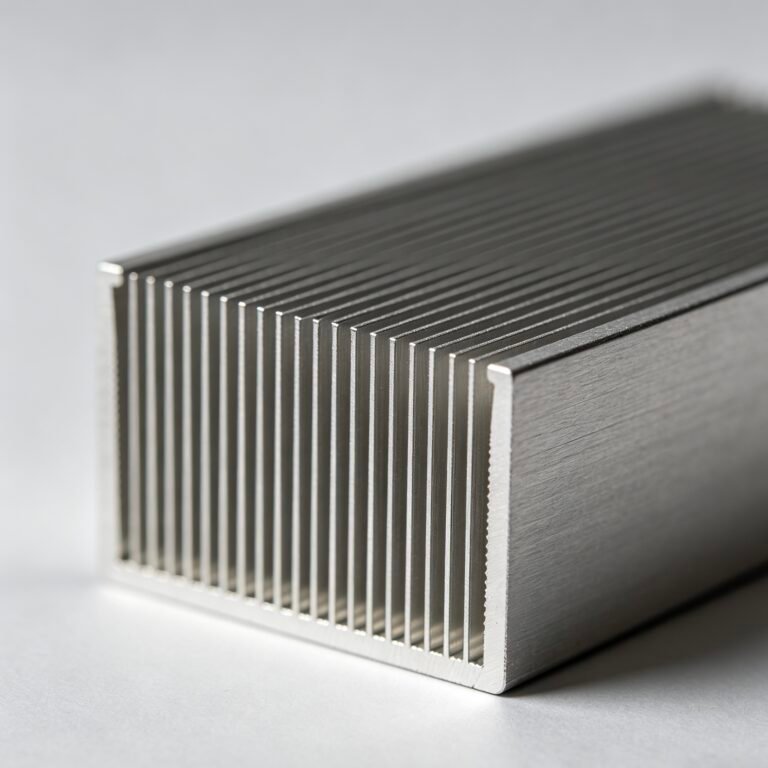
Choosing a 2020 aluminum extrusion is not simply a matter of specifying a 20 × 20 mm profile. Slot geometry, wall thickness, alloy, surface finish, cut tolerance, and fastener compatibility can all affect assembly and production cost.
When designing modular frames, 3D printers, or automation equipment, the 2020 industrial aluminum extrusion profile remains an industry standard. However, even experienced engineers often fall into subtle specification traps. Selecting the wrong profile variants or mismatched tolerances can cause structural instability, assembly delays, and unnecessary expense.
As a dedicated aluminum extrusion profile manufacturer and global supplier- Vanway Tech frequently helps clients‘ technical teams troubleshoot these exact engineering mistakes. Below are the most common specification errors to avoid before placing your next factory order.
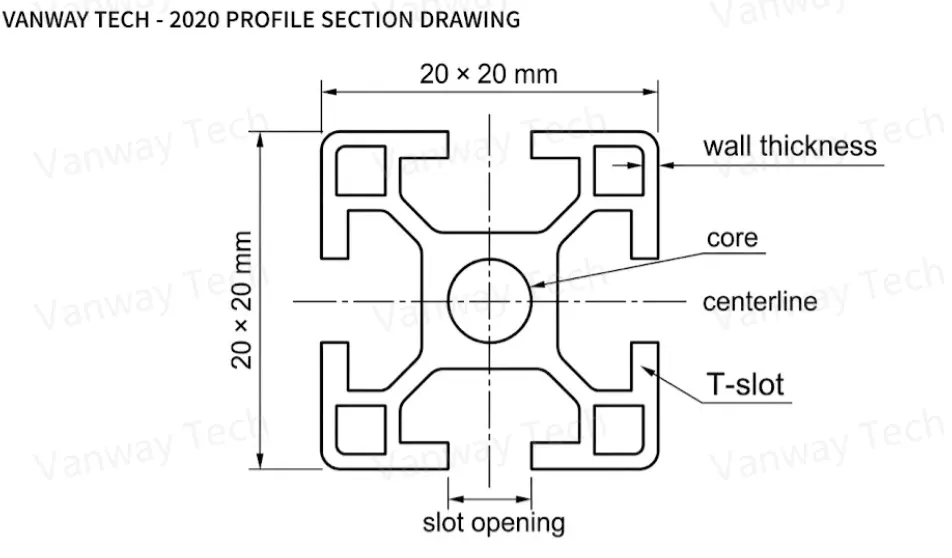
This guide covers seven specification mistakes we commonly see when reviewing 2020 aluminum extrusion requirements and explains what buyers should confirm before placing an order.
1. Specifying Only the 20 × 20 mm Overall Size
Saying you need “2020 aluminum extrusion” is a good start, but it’s nowhere near enough information for a factory to go on. Outside dimensions only tell half the story. Two profiles can both sit at 20 × 20 mm on a caliper, yet feature entirely different slot openings, wall thicknesses, internal web geometries, and corner radii. If those details don’t match your design, your T-nuts won’t drop in, your frame will lack structural rigidity, or your end connectors simply won’t line up.
Before signing off on a purchase order, always insist on reviewing and approving the complete CAD cross-section drawing—never rely on the nominal size alone.
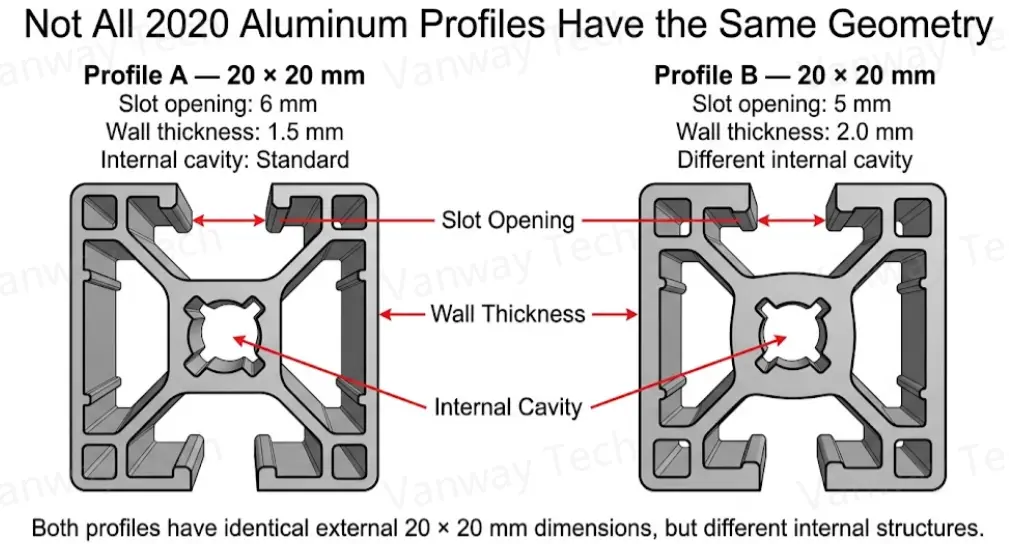
2020 T-slot Aluminum Extrusion Inspection Checklist for Buyer:
| Inspection Item | Verification Focus & Action |
|---|---|
| Overall dimensions | Confirm outer height, width, and corner radii tolerances. |
| Slot opening | Verify slot width (e.g., 6 mm vs. 8 mm) and depth for T-nut drop-in clearance. |
| Wall thickness | Check outer and internal wall gauges to ensure the profile meets load requirements. |
| Internal geometry | Review core hole diameter (for tapping) and internal rib structure. |
| Profile weight | Compare linear mass (kg/m or lbs/ft) against your structural load calculations. |
| Fastener compatibility | Double-check fitment with target hardware (M5/M6 T-nuts, corner cubes, roll-in spring nuts). |
2. Choosing the Wrong T-Slot or V-Slot Geometry
Honestly, if you’re building a 3D printer or a desktop CNC, the single easiest way to mess up your 2020 frame ordering is mixing up T-Slot Aluminum Extrusion and V-Slot Aluminum Profiles.
On paper, both are 20mm × 20mm aluminum extrusions with center channels, but the bevel on the slot edges makes them completely different tools for the job.

T-Slot Aluminum Extrusions (Standard T-Groove)
The channel edge on a T-Slot is 90° square with flat, vertical walls inside the slot.
- What it’s for: Purely structural framing and rigid joins.
- Hardware: T-nuts (drop-in or roll-in) and standard M5 screws to clamp corner brackets and plates down tight.
- Real-world feel: Rock solid for building machine frames, enclosures, or workbenches. It’s cheap, rigid, and everywhere.
- The trap: Don’t try rolling V-wheels inside a T-Slot channel. Because the edges are square, the wheel sits on a sharp edge instead of resting flush. It’ll chew up your Delrin/POM wheels, spray plastic dust everywhere, and bind up instantly.
V-Slot Aluminum Profiles (V-Groove)
V-Slot takes the standard profile and adds a 45° angled bevel along the inner lips of the slot.
- What it’s for: Dual-purpose—it handles structural framing AND doubles as a linear motion rail.
- Hardware: Dual V-wheels (POM or steel). The angled profile of the wheel locks right into the 45° chamfer, tracking smooth and straight like a train on a track.
- Real-world feel: This is what budget printers like the Ender-3 use for X, Y, and Z travel to avoid paying for pricey steel linear rails.
- Compatibility note: V-Slot accepts almost all standard T-slot nuts and brackets, but T-Slot cannot run V-wheels.
T-Slot vs. V-Slot Aluminum Profiles Comparison:
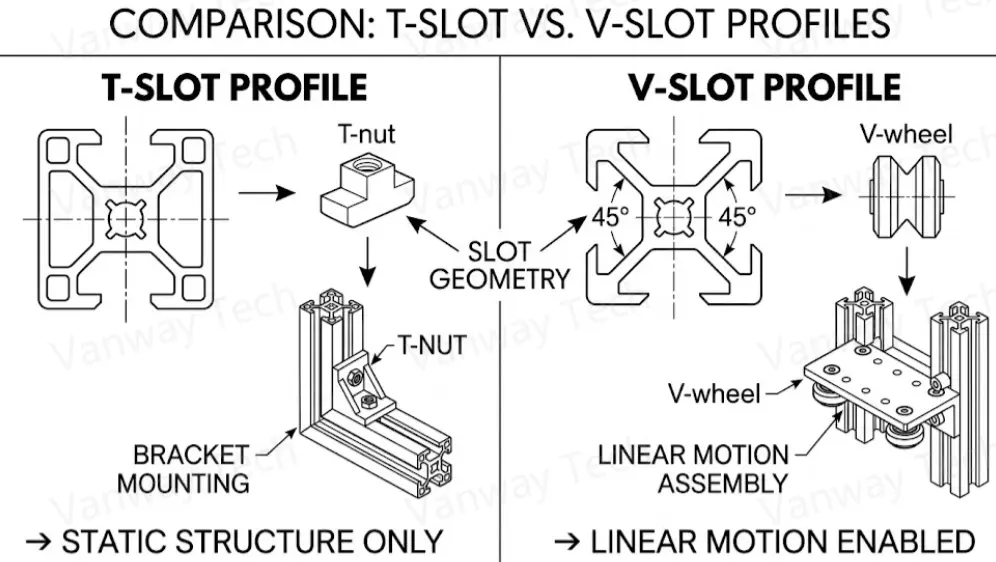
T-Slot vs. V-Slot Aluminum Profile Which one should you buy?
It comes down to one practical rule:
- If anything needs to slide along the extrusion using POM wheels: You must get V-Slot. No debate here.
- If you’re just building a rigid frame, enclosure, or stand where nothing rolls directly on the profile: Go with T-Slot. It’s cheaper, slightly more rigid, and easier to source in bulk.
Quick tip if you plan to mount metal linear guide rails (like MGN12) directly onto the aluminum: either profile works fine. Since the rail handles the smooth motion and the extrusion is just a flat backing, saving a few bucks with standard T-Slot is usually the smart play.
3. Ignoring Wall Thickness and Profile Weight
Why 2020 Industrial Aluminum Profile Weight Matters?
Just because two aluminum profiles share a 20 × 20 mm footprint doesn’t mean they’ll handle the same job. Extruders can easily shave down wall thicknesses and hollow out internal webs to cut material costs, but saving a few cents on a lightweight profile will quickly backfire if your machine frame starts twisting or flexing under load.
Before you lock in your bill of materials, take a hard look at how the profile’s physical build matches up with the actual forces it will experience in the field.
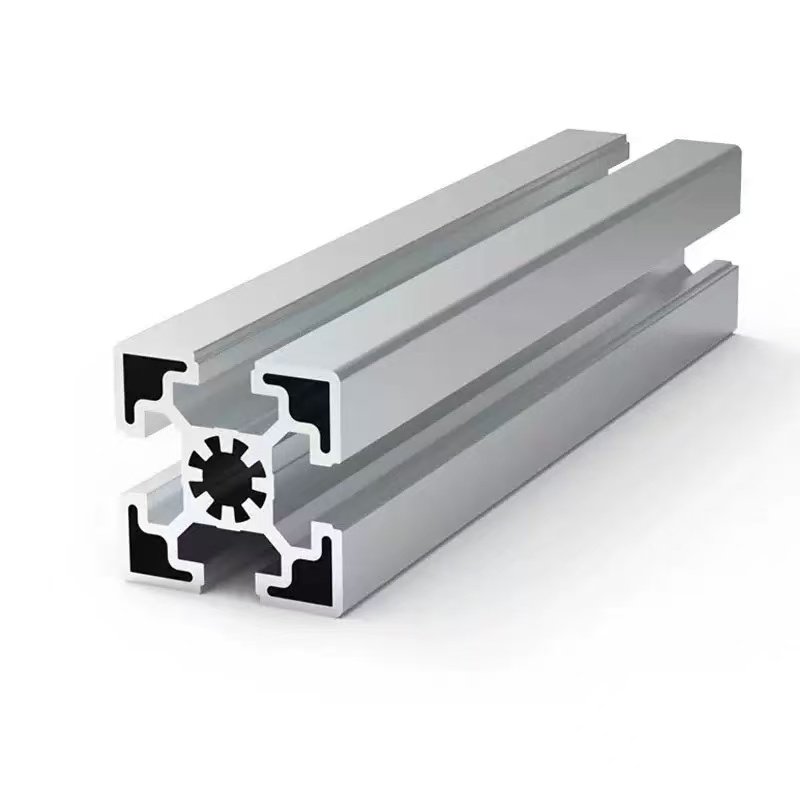
Light Duty 2020 T-slot Aluminum Frame for Display Stands
Structural Load Evaluation Checklist:
- Wall thickness: Inspect both outer walls and internal webs to ensure they can handle clamping forces without crushing or buckling.
- Weight per meter: Compare linear mass (kg/m or lbs/ft) to balance structural rigidity against overall machine weight.
- Unsupported span: Factor in the length of any unbraced profile runs—longer spans require beefier cross-sections to prevent sagging.
- Applied load: Account for static weights, motor torque, and dynamic forces like gantry acceleration.
- Deflection requirement: Determine how much structural flex your application can tolerate before precision, alignment, or part quality suffers.
4. Selecting Alloy and Temper Only by Strength
Don’t Default to 6061-T6: Choosing the Right Alloy and Temper for T-Slot Aluminum Extrusion
It’s easy to assume that picking a higher-yield alloy like 6061-T6 will automatically make your 2020 profile better. In reality, cranking up material strength often comes at the expense of surface finish, extrusion precision, and cost.
For the vast majority of 2020 extrusion applications, 6063-T5 is the sweet spot. It extrudes much cleaner, allowing for intricate internal wall geometries and tighter slot tolerances. More importantly, it yields a smooth, uniform surface finish that takes anodizing exceptionally well—critical if your frame is visible on an end product.
6061-T6, on the other hand, gives you higher tensile and yield strength alongside better machinability (like post-extrusion tapping or milling). But it’s stiffer to push through an extrusion die, which limits how thin or complex your internal web walls can be without driving up tooling costs.
Always balance mechanical strength against cosmetic requirements and manufacturing feasibility before locking in your material spec.

Quick Alloy Comparison for 2020 T-Slot Aluminum Extrusion
| Requirement | 6063-T5 | 6061-T6 |
| Complex Extrusion Geometry | Excellent (ideal for thin webs and fine detail) | More demanding (harder on dies, looser tolerances) |
| Surface Appearance | Excellent, smooth out of the die | Good, can show minor die lines |
| Anodizing Finish Quality | Premium, high uniformity | Good, functional finish |
| Mechanical Strength | Moderate | Higher tensile and yield strength |
| Primary Applications | Standard framing, enclosures, architectural runs | High-load structural parts, heavy machining |
5. Not Defining Surface Finish Requirements for T-Slot Aluminum Extrusions
Simply writing “anodized aluminum” on a purchase order leaves way too much room for interpretation. Anodizing ranges from thin decorative coatings to thick hardcoats, and without explicit specs, you might end up with uneven shading, improper corrosion protection, or a matte finish when you expected gloss.
For 2020 extrusions, cosmetic appearance is often just as important as structural performance—especially when building exposed machine frames, display enclosures, or consumer-facing products. Beyond specifying the finish process and color, you need to account for anodizing layer thickness and batch-to-batch color consistency. Aluminum extrusions processed in different anodizing tanks or separate production runs can exhibit subtle shade variations that stand out instantly when assembled side by side.
Define your finish expectations completely up front to avoid costly rejections.
Surface Finish Checklist for T-Slot Aluminum Extrusion
| Inspection Item | Specification & Requirement |
|---|---|
| Finish Type | Specify whether you need mill finish, clear/black anodized, or powder coated. |
| Color & Tone | Define exact color codes (e.g., Matte Black vs. Satin Silver) rather than generic names. |
| Gloss Level | Indicate desired reflectivity (e.g., high gloss, satin, or matte/bead-blasted). |
| Anodizing Coating Thickness | Specify film thickness based on environment (e.g., 10 µm for indoor decorative use vs. 15–25 µm for harsh or outdoor environments). |
| Visual Acceptance Criteria | Set clear inspection standards for visual defects like die lines, rack marks, or handling scratches. |
| Batch-to-Batch Consistency | Require color-matching tolerances (Delta E limits) or limit sample approvals across multiple extrusion lots. |
How to Choose Aluminum Profiles for Coastal & High-Salt Environments:Anodized,PVDF or Powder Coating
6. Treating Cut Length as the Only Machining Requirement
Getting the overall length right is only step one. A profile can be cut to the exact millimeter, but if the end cut isn’t perpendicular or the edges are left jagged, your entire frame will throw off alignment during assembly. Out-of-square cuts introduce gaps at corner joints, causing machine frames to twist, bind linear motion rails, or wobble under load.
Beyond cut precision, relying on your own shop floor to handle post-extrusion work—like end-tapping core holes, drilling access ports, or milling slot drop-ins—wastes valuable assembly time. Specifying these secondary operations directly with the extrusion supplier guarantees factory precision and speeds up final production.
Always define the complete machining scope on your technical drawings before releasing a order.
Secondary Machining Workflow Checklist:
- Cut Length & Tolerance: Specify linear cutting tolerances (e.g., ±0.2 mm) based on overall frame assembly needs.
- End Squareness (Perpendicularity): Set strict squareness limits (e.g., ≤ 0.5° or within 0.1 mm across the profile width) to prevent racking at corner joints.
- Tapping & Core Threading: Indicate core hole thread sizes (e.g., M5 or M6 thread depth) for direct blind-joint bolting.
- Drilling & Access Holes: Detail position, diameter, and counterbore specs for internal wrench access or through-bolt fastening.
- Slotting & Milling: Specify keyway notches, end-milling, or drop-in slot modifications required for hidden mounting hardware.
- Deburring & Edge Finishing: Require full edge deburring and chip removal to protect operators, preserve anodizing quality, and ensure flush mating surfaces.
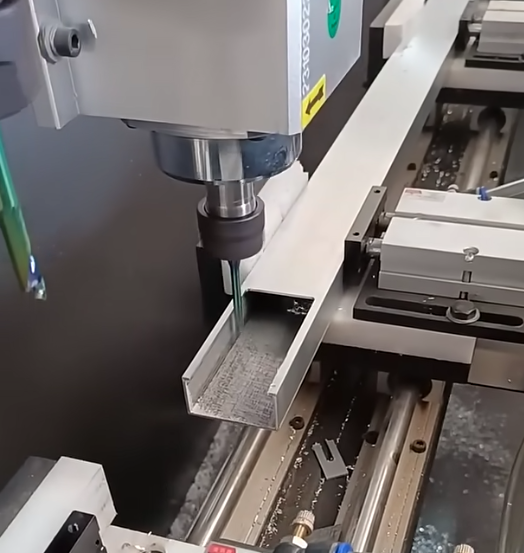
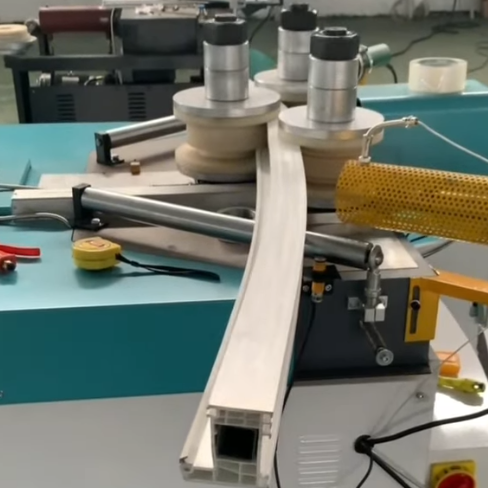
Aluminum Extrusion Processing Capability – Vanway Tech
7. Forgetting Fastener Compatibility
Even perfectly extruded aluminum is useless if your hardware won’t fit the slot. Matching fasteners to profile geometry seems obvious, but it remains one of the most common procurement oversights.
Slot openings (typically 5 mm vs. 6 mm), channel depths, and internal shoulder angles vary across 2020 Aluminum profiles. A roll-in nut or corner bracket designed for one slot geometry will jam or sit loose in another.
To avoid shop-floor rework, Vanway Tech recommends cross-referencing your profile drawing with your hardware specs before approving production.
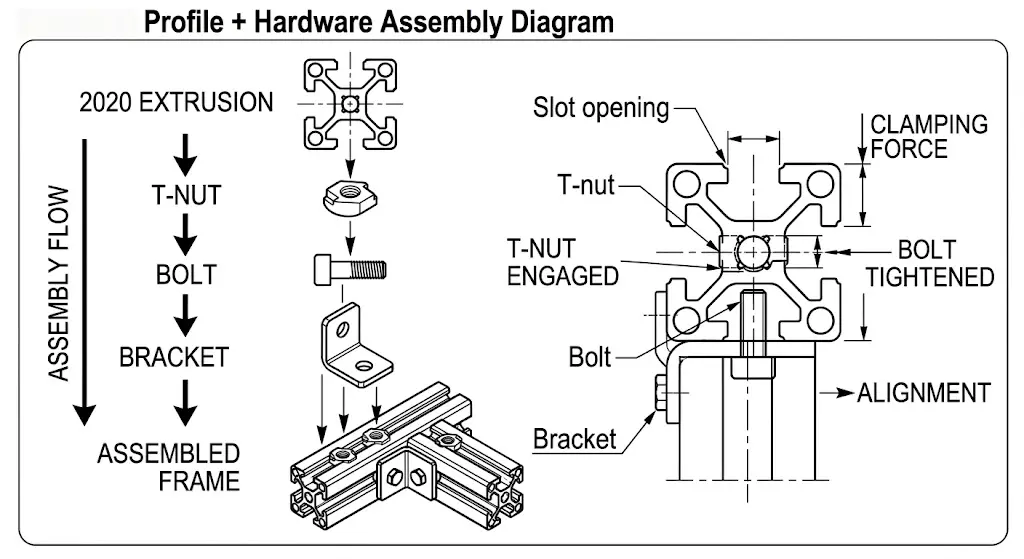
Compatibility Checklist:
- Slot Width: Ensure T-nuts and spring nuts match the exact opening (5 mm vs. 6 mm).
- Slot Depth: Confirm internal shoulder depth allows nuts to lock flat without bottoming out.
- Bracket Alignment: Verify corner brackets and connector tabs align with the profile’s slot width.
- Core Hole Tapping: Check central core hole size for target end-bolts (e.g., M5 or M6).
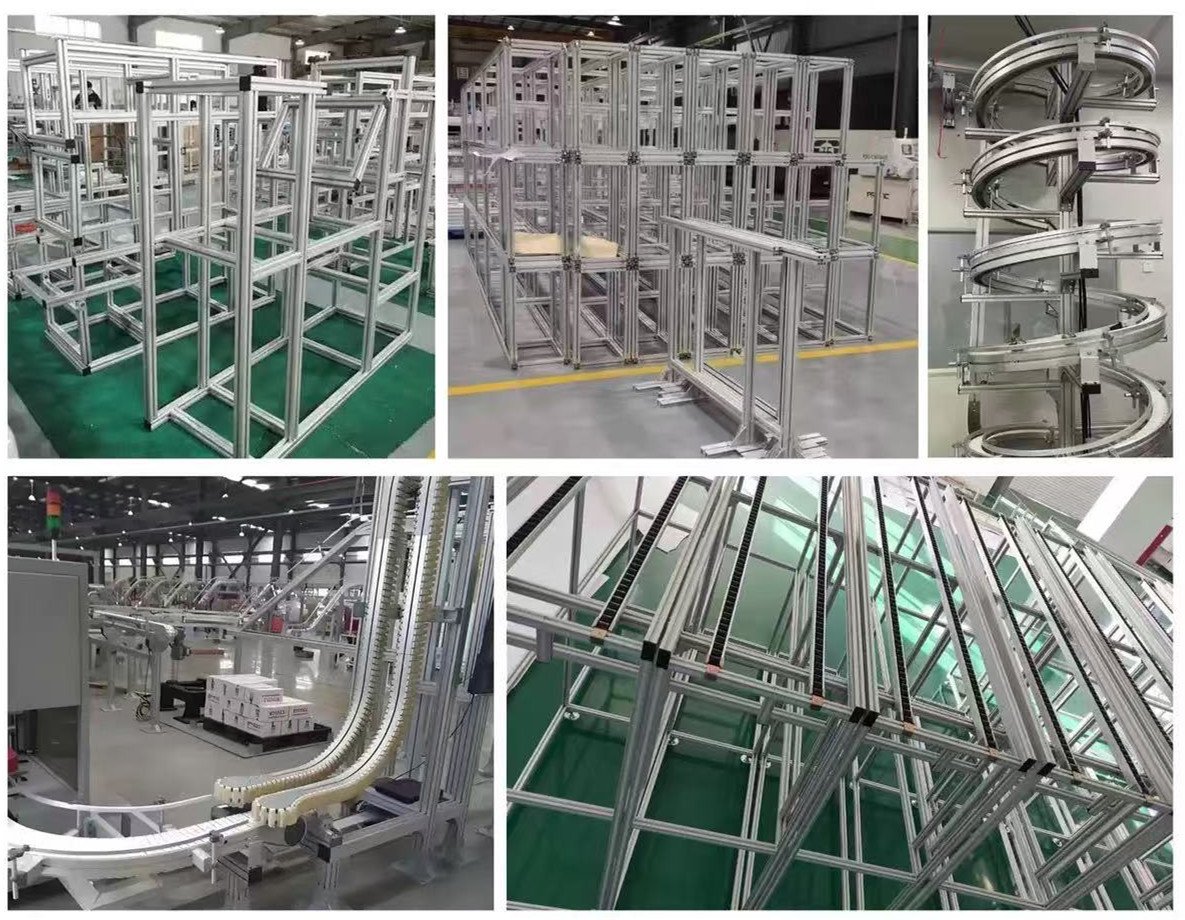
2020 Aluminum Extrusion Specification Checklist
Before requesting a quotation (RFQ), buyers should clarify and provide the following technical parameters to ensure accurate pricing, proper fitment, and reliable structural performance.
| Specification Parameter | What to Confirm / Requirement Standard |
|---|---|
| Profile Size | 20 × 20 mm nominal cross-section |
| Slot Geometry | T-slot (structural) / V-slot (linear motion chamfer) |
| Slot Opening | Throat width dimension as per cross-section drawing (e.g., 5 mm vs. 6 mm) |
| Alloy & Temper | 6063-T5 (cosmetic/intricate) or 6061-T6 (high mechanical strength) |
| Wall Thickness | Outer wall & inner web thickness matching drawing rigidity requirements |
| Profile Weight | Target linear mass (kg/m) to balance strength against material cost |
| Length Specifications | Required stock length or custom cut length |
| Tolerances | Linear cutting length tolerance (±mm) & end-face squareness (perpendicularity) |
| Surface Finish | Anodized (clear/black), powder coated, or mill finish |
| Color & Appearance | Clear silver, black, or custom color code with batch consistency limits |
| Secondary Machining | Drilling access holes, end-tapping core holes, slotting, or custom cutting |
| Hardware Fitment | Matching fastener specs (e.g., M5/M6 T-nuts, bolts, gussets, brackets) |
| Order Quantity | Trial order, batch production, or annual volume projections |
2020 Aluminum Extrusion RFQ
Spec Sheet Sample
Profile:
20 × 20 mm
Alloy:
6063-T5
Finish:
Black Anodized
Length:
Custom Cut
Machining:
Drilling + Cutting
Hardware:
M5 T-Nut Compatible
Quantity:
How Vanway Tech Helps Buyers Avoid Specification Errors?
Vanway Tech reviews every aluminum profile specification before production to verify cross-section geometry, alloy selection, surface finishes, tolerances, and hardware compatibility.
An auto parts manufacturing factory in Indonesia submitted a 20×20 mm profile inquiry specified purely by outer dimensions.
During Vanway Tech’s standard drawing review, our engineering team flagged several hidden mismatch risks: the inner wall geometry was too light for their span load, the slot opening was 5 mm while their intended roll-in nuts required 6 mm, and the anodizing spec lacked batch color consistency targets.
We adjusted the profile web thickness, aligned the slot dimensions with their target hardware, and locked in a 15 µm anodizing standard before cutting tooling. Resolving these parameters up front saved the client from costly mold re-tooling, mismatched fastener stock, and assembly delays on the factory floor.
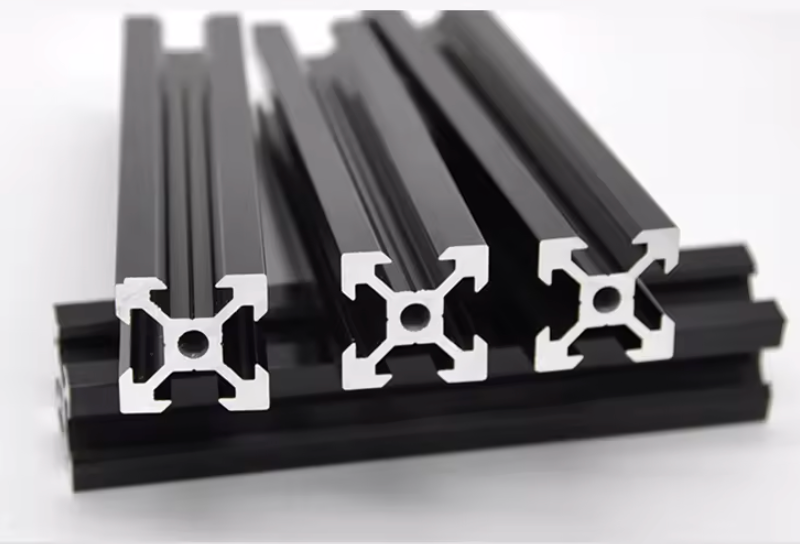
Whether you bring a complete CAD drawing, a physical sample, or just a rough application concept, our engineering team conducts a thorough DFM (Design for Manufacturability) audit. We identify potential assembly bottlenecks—such as slot mismatches, wall deflection, or improper anodizing callouts—before you invest in tooling or bulk extrusion runs. By aligning profile geometry with your actual mechanical load and fastener ecosystem, we ensure seamless assembly and batch-to-batch consistency from day one.
Vanway Tech 丨 The Professional and Trustable Factory of T-Slot Aluminum Extrusion from China
Avoiding these mistakes is much easier when you consult directly with the factory floor rather than third-party distributors.

As a trusted industrial aluminum profile manufacturer and direct supplier – Vanway Tech provides complete end-to-end support:
- Custom Die Design & Precision Extrusion
- Precision CNC Machining, Tapping, & Mitering
- Strict Quality Control and Dimension Inspections
- Custom Packaging for Safe Global Shipping

Ready to Optimize Your Profile Specifications?
Don’t let minor specification errors slow down your production schedule.
Contact our technical engineering team at Vanway Tech today to request detailed CAD files, profile load charts, or a direct factory quote.
FAQs of 2020 Industrial Aluminum Profile
Q1. Can Vanway Tech customize a 2020 aluminum extrusion profile?
A: Yes. Vanway Tech can develop custom 2020 profiles based on drawings, samples, or application requirements.
Q2. Which alloy is better for a 2020 aluminum extrusion?
A: It depends on the application. 6063-T5 is often suitable for complex profiles and surface-finish requirements, while 6061-T6 may be considered when higher strength is required.
Q3. How should I specify a 2020 aluminum extrusion for quotation?
A: Provide the profile drawing, alloy and temper, length, surface finish, machining requirements, hardware requirements, and estimated quantity.
Q4. Can Vanway Tech supply cut-to-length 2020 profiles?
A: Yes. Cut length and secondary machining can be specified according to the production drawing.
Q5. How can I avoid ordering incompatible T-nuts?
A: Confirm the slot opening and internal profile geometry against the T-nut manufacturer’s dimensions before ordering.
Related Posts You May Interested In


Contact With Vanway Tech Team for Premium Aluminium Extrusion Products!
Enquire with UsConnect with Vanway Tech Team for Premium Aluminium Extrusion Products.
Contact InfoWe are looking forward to hearing from you!
-
Email: info@vanway-tech.com
-
Address: No. 588, Wuyi South Road, CSJ Moldware Town, Wujin, Changzhou, Jiangsu, China
Scan Below Codes to Contact Us Immediately.