Vanway Precision Materials Tech Co.,Ltd
How to Verify Primary vs. Recycled Aluminum Extrusions
Primary vs Recycled Aluminum Extrusions Profiles: Spot the Difference Fast | Vanway Tech
Table of Contents
Sourcing custom aluminum extrusions seems simple at first—submit a CAD model, select an alloy grade, and compare bids. However, the lowest quote often conceals critical quality shortcuts. Using unapproved scrap or reducing wall thickness leads directly to corrosion, poor assembly, and sudden structural failures in final production.
Whether you work in aluminum profiles for solar racks, EV battery trays, high-rise curtain walls, or automation frames, spotting these supplier traps early is critical. It’s the only way to protect your product quality—and your bottom line.
When buying custom aluminum extrusions, it is not enough to ask whether the material is “primary” or “recycled.” Buyers need to verify the alloy, chemical composition, material source, traceability, and finished-profile quality before production.
This guide explains a practical three-step process for checking aluminum material without relying on appearance alone.

What Is Primary A00 Aluminum?
For aluminum extrusion buyers, primary aluminum, A00 aluminum, and 6063 or 6061 alloy are not the same thing. Primary aluminum describes the material source, A00 commonly refers to a high-purity unalloyed aluminum ingot designation, while 6063 and 6061 are wrought aluminum alloy designations used for products such as extrusions.
Primary Aluminum /
A00 Ingot
A00 Ingot
A00 / Al99.70 — primary unalloyed aluminum
→
Aluminum Billet
Billet — extrusion feedstock
→
6063-T5 / 6061-T6
Extrusion
Extrusion
6063 / 6061 — alloy designation
T5 / T6 — temper
T5 / T6 — temper
What Does A00 Mean in Aluminum Extrusion Procurement?
In the Chinese aluminum market, A00 is commonly used for primary unalloyed aluminum corresponding to Al99.70, with a minimum aluminum content of 99.70% under the referenced GB/T 1196 designation.
For buyers, however, an A00 label is not enough to verify the material used in a finished extrusion. Check the MTC or COA, chemical composition, heat or batch number, and applicable material standard. If primary or recycled content is a contractual requirement, ask for supporting material-source and traceability records.
Is A00 Aluminum the Same as 6063 or 6061?
No. A00 refers to high-purity unalloyed aluminum, while 6063 and 6061 are alloy grades. The 6xxx series uses alloying elements such as magnesium and silicon to achieve specific processing and performance characteristics.
For extrusion purchasing, specify the material in this order:
Material source → alloy → temper → extrusion requirements → inspection
For example, 6063-T5 and 6061-T6 have different alloy and temper requirements. The A00 designation alone does not tell a buyer whether a finished profile meets either specification.
| A00 | 6063 | 6061 |
|---|---|---|
| Primary unalloyed aluminum | Wrought alloy | Wrought alloy |
| Al99.70 | Al-Mg-Si | Al-Mg-Si |
| Raw material designation | Common extrusion alloy | Higher-strength extrusion alloy |
A00 aluminum ingots / aluminum billet with heat number / 6063 billet / finished 6063 extrusion
Why Primary Aluminum Does Not Automatically Mean a Better Extrusion?
Primary aluminum is only one factor in extrusion quality. The finished profile also depends on alloy chemistry, billet quality, extrusion conditions, heat treatment, die design, dimensional control, and surface finishing.
Recycled aluminum is not automatically lower quality either. When properly processed and controlled, recycled material can be used to produce billet that meets the required alloy specification.
For B2B buyers, the more useful question is:
Does the billet and finished extrusion meet the specified alloy, temper, mechanical, dimensional, and surface requirements?
If primary aluminum is required for a specific project, state it clearly in the purchase specification and request the relevant material documentation and traceability records.indicates lower quality.
Primary vs. Recycled Aluminum Extrusions: What Should You Actually Verify?
For aluminum extrusion buyers, the key question is not simply whether the material is primary or recycled. The finished billet and extrusion should meet the specified alloy, chemical, mechanical, and dimensional requirements. Verify these four areas before production.
PRIMARY OR RECYCLED?
Material source is only one part of extrusion quality.
| No. | Category | Details / Process Flow |
|---|---|---|
| 01 | Material Source | Primary / Recycled / Specified Blend |
| 02 | Alloy & Chemistry | 6063 / 6061 / Chemical Composition |
| 03 | Traceability | Billet → Heat/Lot → Production Batch |
| 04 | Finished Quality | Mechanical Properties → Dimensions → Surface |
Alloy and Chemical Composition
Confirm the specified alloy, such as 6063 or 6061, and check its chemical composition against the applicable standard. The MTC or COA should provide the alloy designation and relevant elemental data. When material source matters, request supporting documentation rather than relying on appearance.
Billet Source and Material Traceability
Ask whether the billet is made from primary aluminum, recycled aluminum, or a specified blend when required by the project. Heat, lot, or batch numbers should link the raw material records to the extrusion production batch.
Mechanical Properties and Temper
Verify the required temper, tensile strength, yield strength, and elongation for the specified alloy. For example, 6063-T5 and 6061-T6 have different mechanical requirements, so material source alone is not enough to determine performance.
Dimensional and Profile Requirements
Check wall thickness, profile dimensions, straightness, cut length, and other critical tolerances against the approved drawing. These requirements determine whether the finished extrusion is suitable for the intended application.
Can You Identify Recycled Aluminum by Appearance?
Not reliably. Visual inspection is useful for checking surface condition and obvious extrusion defects, but it cannot confirm recycled content, material purity, or the source of the aluminum.
Primary vs Secondary Aluminum Profiles: What Visual Inspection Can or Cannot Tell You?
Look for visible issues such as scratches, dents, pitting, discoloration, die lines, or uneven finishing. You can also compare the profile with the approved sample and surface specification.
Appearance cannot reliably confirm primary or recycled content, alloy composition, or material purity. Similar surface conditions can result from billet quality, extrusion settings, die condition, cooling, handling, or surface treatment.
Why Surface Defects Are Not Proof of Recycled Content?
A surface defect does not automatically mean recycled aluminum was used. Both primary and recycled billets can produce defects when material preparation or extrusion conditions are not properly controlled.
For material verification, use MTC/COA records, batch traceability, supplier documentation, and chemical testing when required rather than appearance alone.
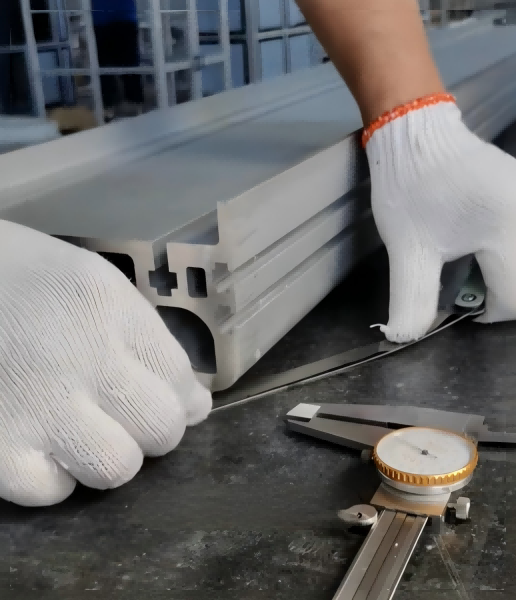
Primary vs. Recycled Aluminum: What You Can Actually Verify?
For aluminum extrusion buyers, the main concern is not simply whether the material is primary or recycled. The important question is whether the billet and finished extrusion meet the specified alloy, chemical, mechanical, and dimensional requirements.

Material Documentation and Alloy Verification
Start with the MTC or COA and confirm the specified alloy, temper, chemical composition, and material identification. For example, A00/Al99.70 refers to a primary unalloyed aluminum designation, while 6063 and 6061 are different wrought alloy designations used for extrusion products.
Billet Source and Traceability
If primary aluminum, recycled aluminum, or a specific recycled-content percentage is required, state it clearly in the purchasing specification. Ask the supplier to provide billet, heat, lot, or batch records that support the material-source claim.
Mechanical and Finished-Profile Requirements
Check the required temper, tensile strength, yield strength, elongation, dimensions, wall thickness, and straightness against the agreed specification. These properties should be verified independently of whether the material is primary or recycled.
What Should Buyers Request?
| Verification | Typical Evidence |
|---|---|
| Alloy & chemistry | MTC / COA / chemical analysis |
| Material source | Supplier declaration / recycled-content documentation |
| Traceability | Billet, heat, lot, or batch records |
| Mechanical properties | Test report / inspection record |
| Finished profile | Dimensional and surface inspection |
The key point: verify the material source through documentation and traceability, and verify extrusion quality through testing and inspection. Do not use appearance alone to determine whether an aluminum profile is primary or recycled.
How to Identify Primary A00 vs Recycled Aluminum Extrusions in 3 -4 Steps?
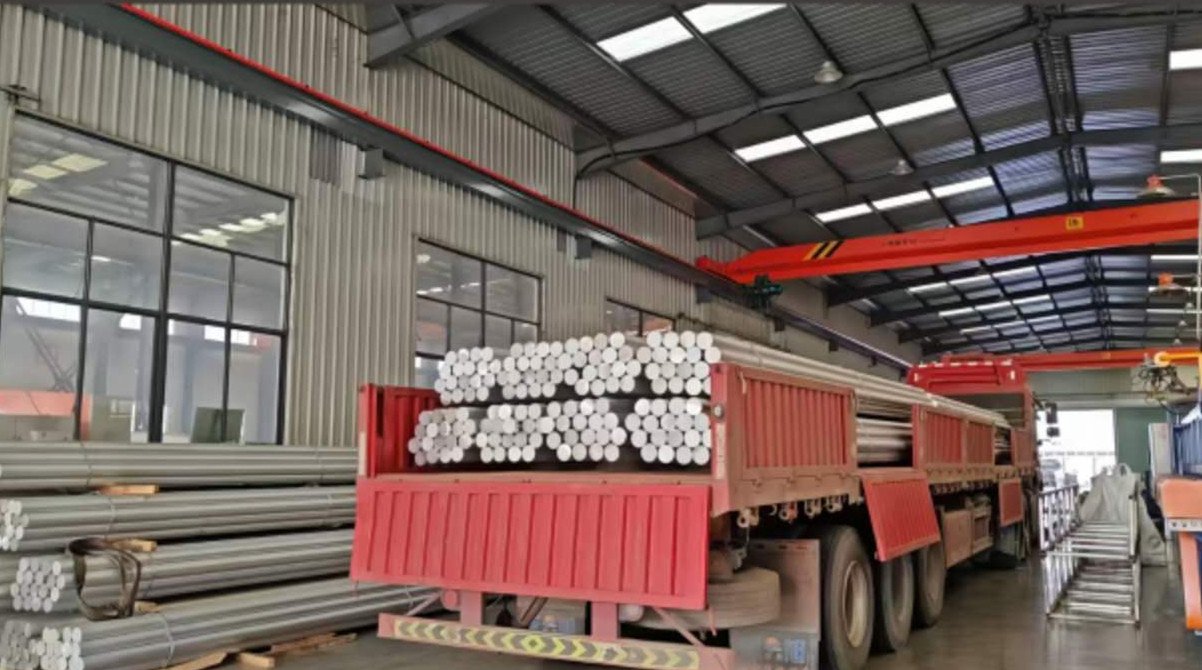
Verification of incoming A00 primary aluminum extrusion profile shipments to ensure purity, mechanical integrity, surface quality, and dimensional compliance prior to warehouse release.

Phase 1: IQC Standard Operating Protocol (SOP)
1.Step 1: Document & Mill Test Certificate (MTC) Verification:Prerequisite before unloading。
- Cross-check shipment packing list against the Purchase Order (PO).
- Inspect the Mill Test Certificate (MTC) for chemical composition. Ensure aluminum purity is 99.70% or higher (A00 grade) and key trace elements comply with standard limits:
- Iron (Fe): 0.35% or lower (Crucial to rule out secondary scrap contamination)
- Silicon (Si): 0.20% to 0.60% (for 6063 alloy)
- Copper (Cu): 0.10% or lower
- Verify ingot batch traceability numbers match physical bundle tags.
2.Step 2: Statistical Sampling & Visual Packaging Audit:ANSI/ASQ Z1.4 (ISO 2859-1) Level II Normal Sampling。
- Perform an external packaging check for moisture damage, broken straps, or transit abrasion.
- Draw random profile samples across top, middle, and bottom sections of selected bundles based on lot size:
- AQL 1.0 for Critical Defects (cracks, structural voids, incorrect alloy)
- AQL 2.5 for Major Defects (out-of-tolerance dimensions, flaking coating, excessive bow/twist)
- AQL 4.0 for Minor Defects (slight surface scratches, minor color variation)
3.Step 3: Physical, Chemical & Mechanical Testing:Execute tests on sampled profiles。
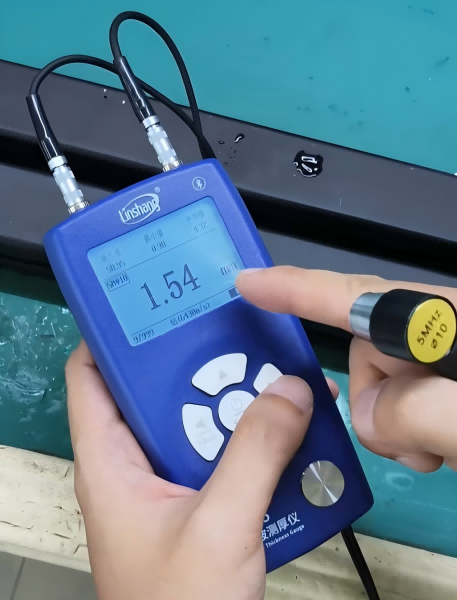
- Visual & Surface Check: Inspect raw bar brightness under 1000 lux illumination. Check for pitting, dark streaks, or die lines.
- Dimensional & Geometric Verification: Measure wall thickness, web dimensions, bow, twist, and angularity against CAD drawings using calibrated calipers and feeler gauges.
- Hardness Testing: Take 5 readings per sample bar using a calibrated Webster Hardness Tester. Target range for 6063-T5: 8 to 12 HW.
- Chemical Spark Spectrometry (XRF): Perform handheld Optical Emission Spectrometry (OES) or XRF testing on cut cross-sections to verify true chemical purity on-site.
4.Step 4: Disposition & Material Tagging:Final gatekeeper sign-off。
- PASS: Apply green “IQC APPROVED” tags to all verified bundles and transfer to main inventory.
- FAIL: Immediately issue a Supplier Corrective Action Request (SCAR), apply red “REJECTED / QUARANTINE” tags, and isolate material in designated non-conforming holding area.
| Inspection Item | Specification / Requirement | Inspection Tool / Method | Acceptance Criteria | Defect Classification |
| Raw Material Purity | Al purity 99.70% or higher (A00 Grade) | MTC Verification / XRF Analyzer | Fe 0.35% or lower; no scrap inclusions | Critical |
| Webster Hardness | 6063-T5: 8–12 HW 6061-T6: 12–15 HW | Webster Hardness Tester | 100% of tested points within range | Major |
| Wall Thickness | Per CAD drawing (e.g., ±0.15 mm tolerance) | Digital Micrometer / Caliper | Zero wall thinning below minimum spec | Major |
| Bow & Twist | Max 1.0 mm per meter length | Flat inspection table & Feeler Gauge | Profiles lay flat without excess warping | Major |
| Cross-Section Cut | Solid, seamless, zero internal voids | Visual 10x Magnifier | Smooth silver glow, no dark grain, no air pockets | Major |
| Surface Finish | Smooth, silver-white luster | Visual inspection under direct light | Free of pitting, black spots, or heavy die lines | Minor / Major |
| Coating Adhesion | ISO Class 0 / ASTM 5B | Cross-Cut Tape Test (1 mm grid) | Zero paint/powder flaking along cut edges | Major |
| Bundle Packaging | Moisture-proof wrapping, wooden skids | Visual / Manual | Intact wrapping, no rust or water spots | Minor |
To ensure consistent quality, an Incoming Quality Control (IQC) protocol is used to verify mill certificates, check material composition via spectrographic analysis, and enforce geometric and physical tolerance standards before production.
What Should an Aluminum Extrusion Supplier Provide?
Before placing an order, buyers should confirm that the supplier can provide the documents and records needed to verify material, traceability, and finished-profile quality.
1. Material Certificates and Test Records
Request an MTC or COA showing the specified alloy, temper, chemical composition, and relevant test results. For critical applications, ask for additional chemical or mechanical test records when required.
2. Billet Source and Batch Traceability
If the project requires primary aluminum, recycled aluminum, or a specific recycled-content level, make this clear in the purchase specification. The supplier should also be able to link the billet, heat or batch number, and extrusion production records.
3. Finished-Profile Inspection Records
Ask how the supplier verifies the final extrusion against the approved drawing. Depending on the project, records may cover critical dimensions, wall thickness, straightness, cut length, and surface condition.
For B2B buyers, the key is traceability: the material documentation should connect to the billet, production batch, and final inspection results.
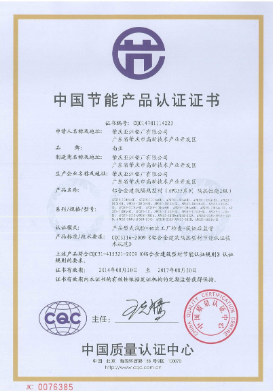
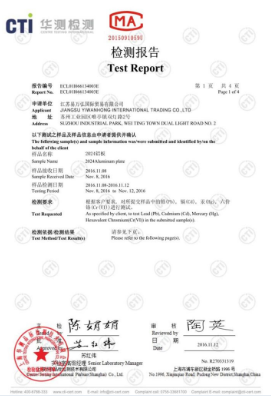
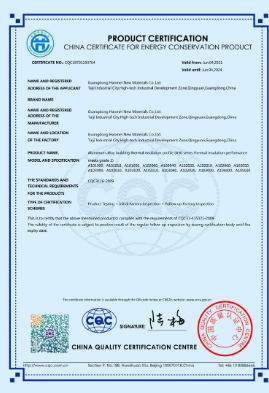
Vanway-Tech丨 Premium Quality Extrueded Aluminum Profiles Manufacturer and Exporter From China Since 2015
Ready to optimize your project? Talk to Vanway Tech engineers and get your custom aluminum extrusion sample started.
Primary vs Secondary Aluminum Profile: How Vanway Tech Verifies Aluminum Material Quality?
Vanway Tech verifies aluminum material and finished extrusions through material documentation, traceability, production control, and final inspection.
Vanway Tech | Aluminum Material & Extrusion Quality Control
| Quality Control Stage | What Vanway Tech Checks | Purpose |
|---|---|---|
| Incoming Material Verification | Alloy, temper, material documentation, and material identification | Confirms incoming aluminum matches the specified material requirements before production |
| Chemical Composition & Alloy Verification | Specified alloy and, when required, chemical composition through additional analysis | Verifies that the material meets the applicable alloy requirements |
| Batch-Level Material Traceability | Billet, heat, lot, and extrusion production batch records | Links raw material documentation to the corresponding production batch |
| Extrusion, Temper & Final Inspection | Extrusion and heat-treatment conditions, critical dimensions, wall thickness, straightness, cut length, and surface condition | Confirms the finished profile meets the approved drawing and specified quality requirements |

Common Aluminum Extrusion Procurement Mistakes
Relying on Appearance to Judge Material Quality
Surface appearance can reveal potential defects, but it cannot prove whether aluminum is primary or recycled. Use documentation, traceability, and testing when required.
Accepting Material Without Traceability
Without clear billet or batch records, it can be difficult to verify material history or investigate a quality issue. Confirm that material documentation can be linked to the production batch.
Comparing Suppliers Only by Price
A lower quote may reflect differences in alloy, tolerances, finishing, testing, packaging, or material requirements. Compare the complete specification rather than price alone.
Failing to Define Material and Inspection Requirements
Specify the required alloy, temper, dimensions, tolerances, surface finish, and inspection requirements before production to reduce misunderstandings and quality disputes.
What You Should Ask Before Ordering Aluminum Extrusions?
Pre-Order Material & Quality Verification Checklist
Before issuing a Purchase Order (PO) for custom aluminum extrusions, confirm these critical material standards with your manufacturer to prevent costly defects and supply risks.
Verification Progress
0 of 5 Completed
| Done | Verification Step & Action Item | Category |
|---|---|---|
1. What Alloy and Temper Will Be Used? Ask the supplier to confirm the exact alloy designation and temper condition (e.g., 6063-T5 for architectural trim or 6061-T6 for high-stress structural profiles) in writing prior to tooling and extrusion production. | Specification | |
2. Can You Provide an MTC or COA? Request the relevant Material Test Certificate (MTC) or Certificate of Analysis (COA). Ensure all documented heat numbers match your specific extrusion batch and chemical/mechanical tolerances. | Compliance | |
3. Can You Provide Batch-Level Traceability? Confirm whether the supplier maintains a full audit log linking the finished extrusions directly back to the original aluminum billet, melt heat, and casting source. | Traceability | |
4. Is the Billet Primary, Recycled, or a Specified Blend? If material origin affects anodizing consistency or end-use performance, state your primary ingot or recycled content percentage strictly in the purchase specification and demand supporting origin declarations. | Sourcing | |
5. Can You Perform Chemical or Mechanical Testing? For load-bearing or mission-critical applications, verify whether the supplier can perform or arrange third-party chemical composition analysis (OES) and tensile/yield strength testing against required standards (e.g., ASTM B221, EN 755). | QA / Testing |
Why Leading Global OEMs Choose Vanway Tech
As an established, vertically integrated precision aluminum profile supplier – Vanway Tech bridges the gap between complex engineering requirements and reliable mass production.
- End-to-End Capabilities: In-house die casting, extrusion mold design, 5-axis CNC deep processing (drilling, tapping, milling), surface finishing, and assembly.
- Industry Expertise: Proven track record delivering structural profiles for Tier-1 automotive suppliers, global solar project EPCs, and premier architectural developers.
- Zero-Defect Commitment: Every shipment undergoes multi-stage inspection to ensure exact alignment with your project’s technical specifications.


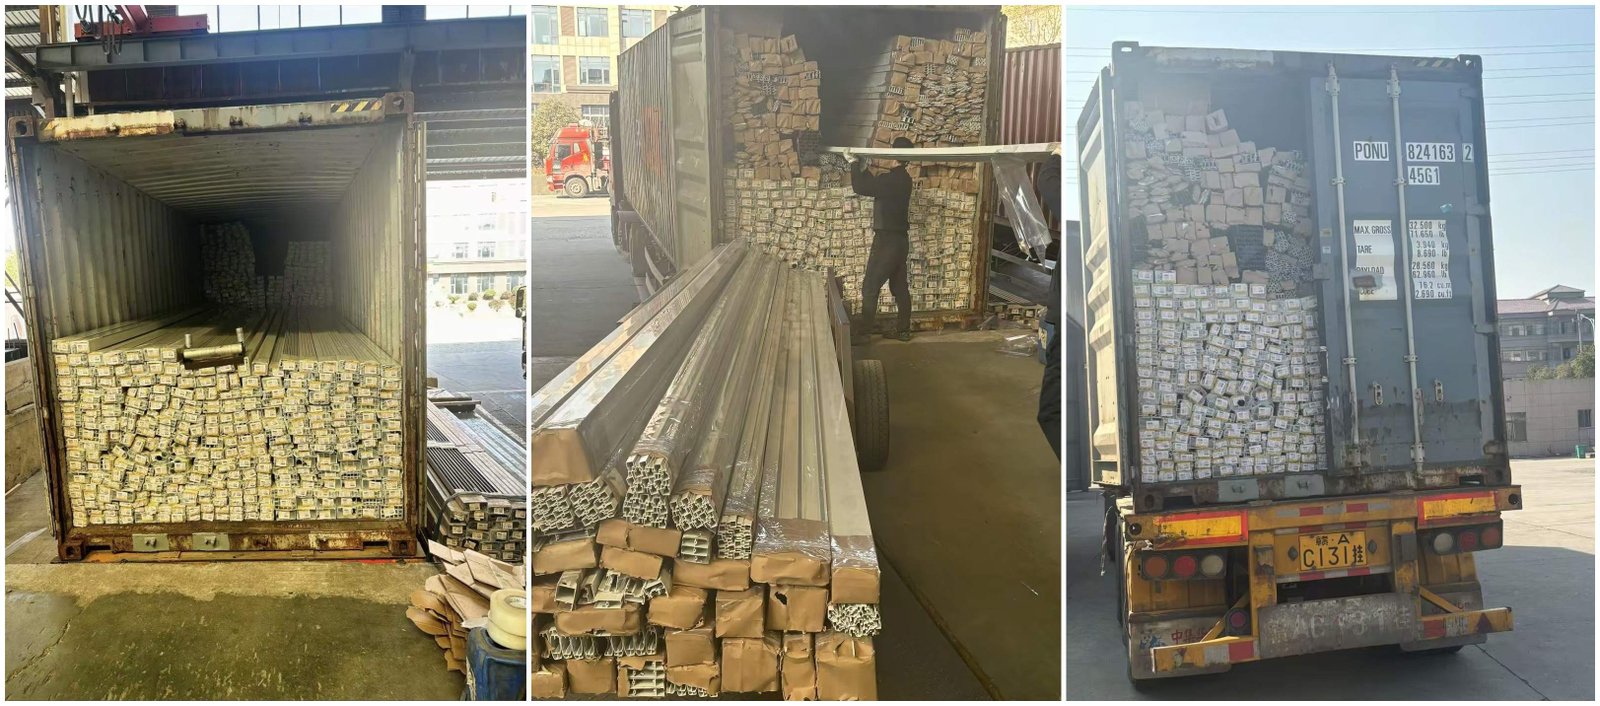
Got Custom Profile Drawings? Get Your Free DFM Analysis in 24 Hours
Eliminate production delays with instant technical validation. Share your 2D/3D CAD files with us now, and our engineering team will deliver a free, comprehensive feasibility review and precision quote within 24 hours—100% free, with zero commitment required.
Related Articals You May Like:
How to make your Aluminum Solar Panel Frame more cost-effective in 2026?
Skived vs. Forged vs. Forged Aluminum Heat Sinks – Sourcing the Right Aluminum Heat Sink
Top-Rated Custom Extruded Aluminum Heat Sink Suppliers in USA & Canada in 2026
How to make your solar module frame aluminum extrusions more cost-effective?
Top 10 Custom PV Module Aluminum Frame Extruders in Gujarat & India (2026)
Contact With Vanway Tech Team for Premium Aluminium Extrusion Products!
Enquire with UsConnect with Vanway Tech Team for Premium Aluminium Extrusion Products.
Contact InfoWe are looking forward to hearing from you!
-
Email: info@vanway-tech.com
-
Address: No. 588, Wuyi South Road, CSJ Moldware Town, Wujin, Changzhou, Jiangsu, China
Scan Below Codes to Contact Us Immediately.